Let’s discuss your container requirements
01708 225350
Call Us
sale@modularmarbles.com
Email Us

7 Best Glass Sorting Machines for Recycling in 2026

Choosing a Glass Sorting Machine is not just a matter of comparing prices or sensor counts. On a busy recycling line, the machine must distinguish clear, green, and amber fragments while dust rises and glass rattles across the conveyor. A small error can send usable cullet into the reject stream. Details matter.

“Accurate sorting begins with a steady feed and ends with a clear quality target.” This is an editorially created observation, not a verified quotation. Alex Morgan is an illustrative process-engineer name, not a cited industry source. A real expert quotation should be confirmed before publication. That distinction matters. Trust depends on evidence, not just confident wording.

This guide reviews seven machines for recycling operations in 2026, with attention to sorting method, throughput, material range, maintenance, and support. Some systems use cameras; others combine optical sensors with air jets that remove unwanted pieces in a blink. The right choice depends on feed consistency, plant layout, and the quality of the recovered glass. A specification sheet cannot reveal every snag. Operators may still face changing contamination, awkward installation, or unexpected downtime. These comparisons offer a useful starting point, not a promise that one machine suits every facility. A site trial can expose the gaps.
7 Best Glass Sorting Machines for Recycling in 2026

What Glass Sorting Machines Do in a Recycling Process

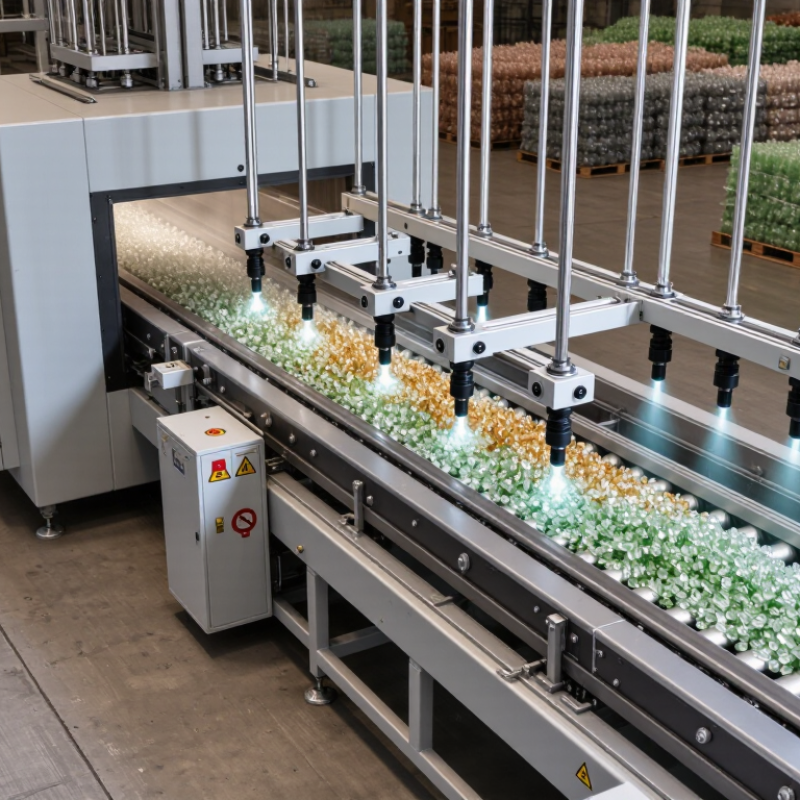
In a recycling process, a glass sorting machine separates broken container glass by color and material. A conveyor spreads the pieces into a shallow, moving layer so sensors can inspect them. Cameras and optical sensors detect differences in color, shape, or surface appearance. When a piece is identified as unwanted, a brief air pulse diverts it into a separate chute. Fast, but not magic. Earlier screens may remove small fragments, while magnets take out some ferrous metal before optical sorting begins.

The sorted glass, called cullet, can be divided into clear, green, and amber streams for further processing. Sorting also helps remove items such as ceramics, stones, and metal fragments, which can affect the quality of new glass. Yet look-alike materials and tiny pieces may escape detection, especially when the feed is dusty or uneven. That matters. A tidy-looking output is not proof of a clean batch. Operators still sample the material, check sensor settings, and adjust the line as incoming glass changes. Sorting machines improve consistency; they do not replace inspection or careful process control.

How Glass Sorting Machines Separate and Classify Materials

Glass sorting machines begin with a steady, shallow feed. Screens remove fines, while magnets pull out ferrous metal before optical sorting. Cameras identify clear, green, and amber pieces by reflected light. Timed air jets then push selected fragments into separate chutes. Small differences matter. A dark label, wet surface, or overlapping shard can confuse detection.

Some systems add X-ray or laser sensors to identify ceramics, stones, and porcelain. These contaminants resemble glass but can weaken new containers during melting. The sensor flags them, and a short air pulse ejects them from the stream. Operators adjust belt speed and sensor thresholds as incoming material changes. No machine reads every fragment correctly.

The U.S. Environmental Protection Agency’s 2018 materials report estimated that 12.3 million tons of glass were generated, with 3.1 million tons recycled—a 25 percent rate. The figure shows why accurate separation matters: usable glass can otherwise leave the recovery stream. Yet higher sorting precision depends on clean feed, regular calibration, and careful checks of rejected material. That last check is easy to neglect. A machine can appear efficient while sending recoverable glass into the reject bin.

Key Technologies Used in Glass Sorting

Glass sorting lines combine imaging, material sensing, and precise mechanical ejection. High-speed RGB cameras inspect each piece as it travels along a conveyor. They identify clear, green, and amber glass by reflected or transmitted light. A steady, shallow layer helps prevent fragments from hiding one another. Small air nozzles then redirect selected pieces into separate chutes.

Different sensors address different contaminants. Near-infrared systems can help distinguish some materials, though clear glass and dark fragments may be difficult to classify reliably. X-ray transmission can reveal density differences, while specialized optical systems help detect ceramics, stones, and porcelain. These contaminants matter: even a small ceramic fragment can compromise a batch of recycled glass. Sensors must be calibrated for fragment size, belt speed, lighting, and dust. Conditions change. A line that performs well with clean cullet may struggle when pieces are wet or heavily mixed. Regular sampling and manual checks remain useful; automated sorting is not infallible. A missed fragment is still possible.

How to Evaluate Glass Sorting Machines in 2026

A glass sorting machine should be judged on your actual feed, not a polished demonstration. In 2026, ask suppliers to run a representative sample that includes clear, green, and amber glass, plus likely contaminants such as ceramics, stones, and labels. Watch the reject stream. A clean-looking output can still hide valuable glass lost to the rejects.

Compare recovery and purity at the same time; improving one may reduce the other. Request results by glass color and contaminant type, then repeat the test with wet or dusty material if those conditions occur at your site. Check rated throughput against your real conveyor speed, not just a peak figure. No test is perfectly tidy; real feed rarely is. That limitation matters.

Look closely at sensor access, calibration steps, and how quickly staff can clear a jam. Ask what routine cleaning involves, how often wear parts need attention, and whether performance data can be reviewed by shift. Estimate energy, labor, and maintenance costs alongside the purchase price. A machine that sorts accurately in a trial may behave differently during a long production run. It is worth leaving room for that uncertainty.

7 Best Glass Sorting Machines for Recycling in 2026 - How to Evaluate Glass Sorting Machines in 2026

The options below are machine configurations, not brand rankings. Sorting results and throughput depend on feed preparation, particle size, contamination, and operating settings; compare suppliers using representative samples of your own material.

Machine configuration How it sorts Best suited for Main advantage Important limitation What to verify in a trial
1. RGB color optical sorter Visible-light cameras classify pieces by color; air jets or mechanical ejectors remove selected fractions. Separating clear, green, and amber container glass after the material has been spread into a suitable layer. Directly targets color fractions that are important in many container-glass recycling processes. Color sorting alone may not reliably remove ceramics, stones, metals, or glass pieces with similar colors. Measure color purity and glass loss for each output fraction using the actual particle-size range and feed mix.
2. Laser-based ceramic, stone, and porcelain (CSP) sorter Laser-based optical detection identifies target contaminants by their optical response; a separation device ejects detected pieces. Removing CSP contaminants from processed glass cullet. Designed to address non-glass mineral contaminants that can remain after basic screening and color sorting. Performance depends on particle presentation, contaminant size, surface condition, and the detection setup. Test removal of representative ceramic and stone pieces, including small contaminants, and record false rejects of saleable glass.
3. X-ray transmission (XRT) sorter X-rays pass through material; the system uses differences in attenuation to identify and separate selected dense contaminants. Applications where density or internal structure helps distinguish contaminants from glass. Can provide information beyond visible surface color. XRT is not a universal solution for distinguishing every glass type or every contaminant; detection depends on material contrast and particle presentation. Ask for test results by contaminant type and size, plus the measured glass recovery and reject rate.
4. Combined RGB and laser CSP sorter Combines visible color classification with laser-based detection in one sorting stage or coordinated stages. Plants that need both color separation and removal of CSP contaminants from cullet. Addresses two different sorting tasks without relying on color detection alone. More sensors and settings can mean higher purchase, integration, and maintenance requirements. Compare each sensor’s contribution separately and check that combined operation maintains the required purity and recovery.
5. Combined RGB and XRT sorter Pairs visible-light color sorting with X-ray transmission analysis for selected density-related separation tasks. Feed streams where color separation and a separately validated XRT target are both required. Combines surface color information with X-ray transmission information. The additional sensor is worthwhile only if it improves separation of contaminants actually found in the plant’s feed. Request side-by-side trials with RGB only and with both sensors enabled, using the same sample and operating conditions.
6. NIR or hyperspectral optical sorter Measures reflected light across selected wavelengths to classify materials based on spectral response. Specialized mixed-material applications where trials confirm a useful spectral difference for the target material. Can add material-class information that a standard RGB camera does not provide. NIR is commonly used for material identification in mixed recycling, but it should not be assumed to distinguish all glass colors or glass contaminants. Require a representative sample trial proving the specific separation task, including results for dirty, wet, or overlapping material if present.
7. Vision-guided robotic picking cell Cameras and image-processing software locate selected objects; a robot removes them with a gripper or other end effector. Removing identifiable large objects or contaminants from a conveyor, rather than high-speed fine-cullet classification. Can target individual objects and may be useful where a discrete pick is more suitable than air-jet ejection. Picking performance is affected by object overlap, conveyor loading, cycle time, and gripper access; suitability for small fragments must be demonstrated. Measure successful picks per operating hour, missed targets, unintended glass picks, and performance at the intended belt loading.

Evaluation checklist: Use the same representative feed sample for each trial. Record feed preparation and particle-size distribution, throughput under stated conditions, product purity, glass recovery, contaminant removal by type and size, compressed-air or energy use, downtime, maintenance needs, and the method used to verify results. Ask suppliers to define each measurement and provide test conditions; there is no single throughput or accuracy figure that applies to every glass stream.

Seven Leading Glass Sorting Machines for Recycling in 2026

Seven Leading Glass Sorting Machines for Recycling in 2026

In 2026, glass recyclers can choose from seven machine types: color optical sorters, ceramic-stone-porcelain detectors, laser sorters, X-ray systems, shape-recognition units, fine-glass separators, and robotic picking systems. Each handles a different challenge.

Color sorters separate clear, green, and amber glass. Ceramic detectors target unwanted fragments that can spoil a batch. Laser and X-ray systems identify material differences, while shape-recognition units assess objects by form. Fine-glass separators process smaller pieces; robotic systems can remove selected contaminants from conveyor belts. Performance depends on feed quality, lighting, belt speed, and careful setup.

Tips: Test your own glass before buying. Ask suppliers to run samples that include labels, moisture, mixed colors, and ceramic fragments. Watch the reject stream, not just the clean output.

A strong line may combine several machine types rather than rely on one unit. For example, screening can remove oversized items before optical sorting, reducing inconsistent feed.

Check recovery rate, purity, maintenance access, and spare-part availability under realistic operating conditions. Results from a polished demonstration may not match a dusty, busy plant. That gap matters.

No sorter catches every contaminant, and settings may need regular adjustment as incoming material changes.

We are proud to support

Registered Company Name: Upminster Containers Limited. Registered Address: Mardyke Works, St Mary's Lane, Upminster, Essex RM14 3PA. Registered Company Number: 00940382
Developed & Maintained By Space Rocket Digital.
chevron-down